Quality & Certification
Empowering Business with Expertise
Pharmaceutical-Grade Packaging
Our packaging products are designed for pharmaceutical and healthcare applications, including dropper bottles, medicine containers, measuring cups and other precision packaging solutions, with a strong focus on product safety, reliability and consistency.
Quality & Safety
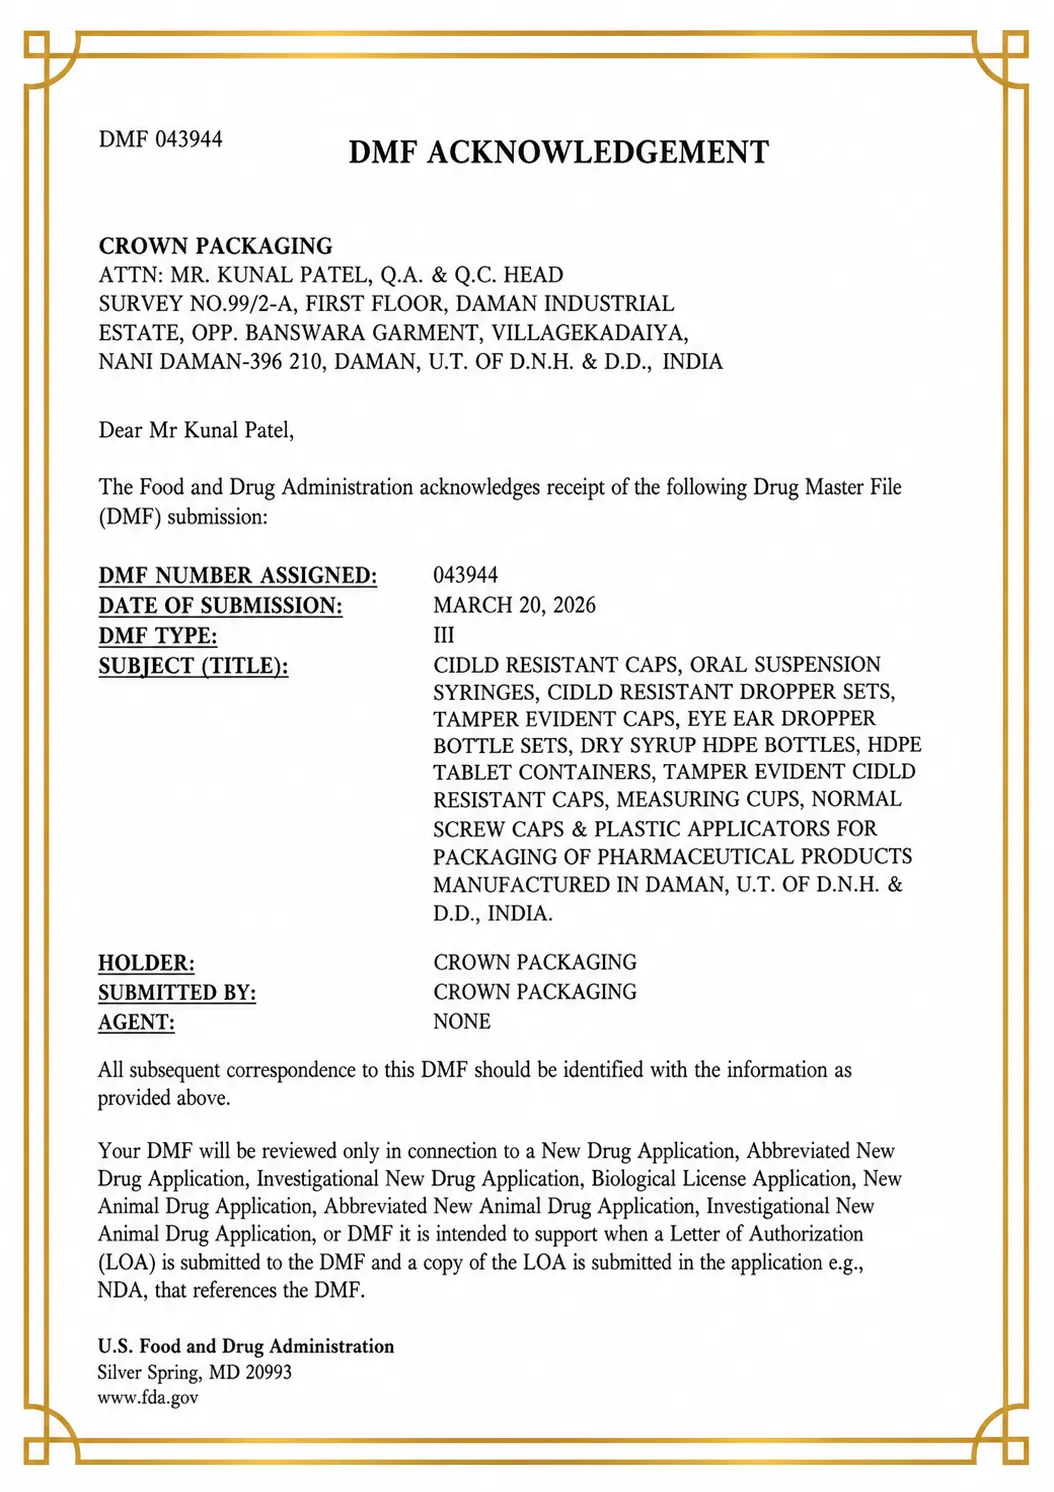
Crown Packaging maintains stringent quality standards throughout the manufacturing process to deliver durable, reliable and application-specific packaging solutions for pharmaceutical and healthcare products.
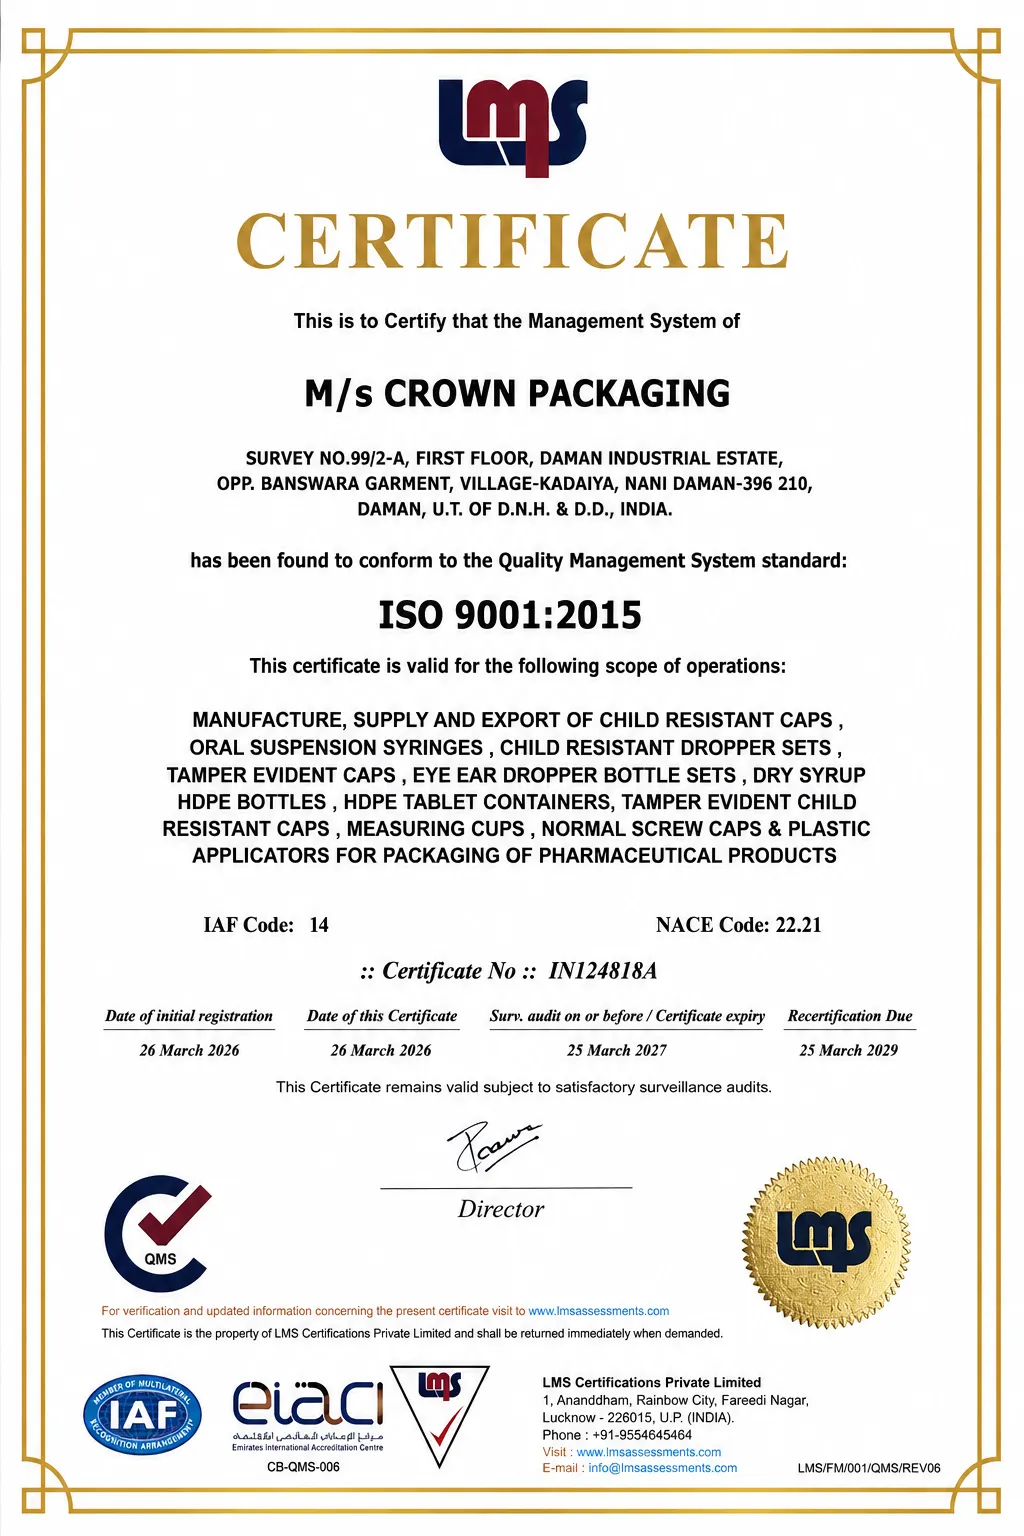
ISO 9001 Certified
Our ISO 9001-certified quality management approach supports consistent manufacturing processes, quality control and continuous improvement, helping ensure reliable packaging solutions for our customers.
Ensuring Quality at Every Stage
Step 01
Continuous Quality Improvement
Driving Excellence Through Ongoing Innovation We continuously review manufacturing processes, quality procedures, and customer feedback to improve product performance, operational efficiency, and overall customer satisfaction while maintaining the highest quality standards.
Step 02
Hygiene & Safety
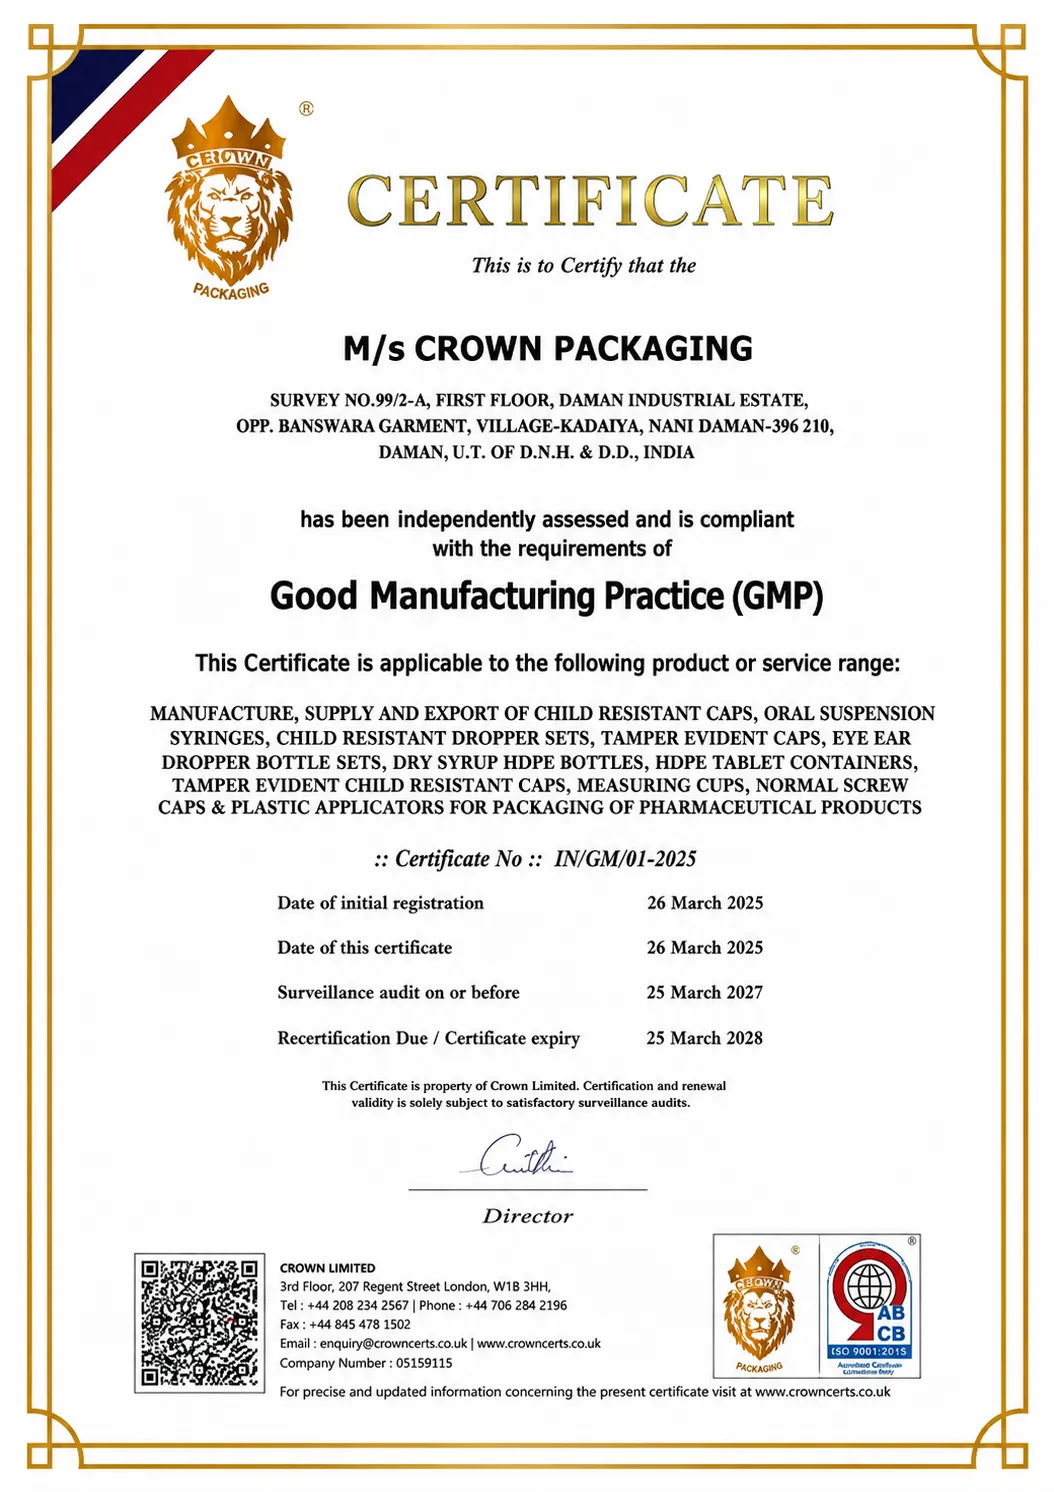
Maintaining a Clean and Safe Manufacturing Environment Production is carried out in hygienic clean room facilities following strict GMP practices, ensuring contamination-free manufacturing and safe handling of pharmaceutical packaging products.
Step 03
Final Product Testing
Every Product Tested Before Dispatch Finished products are thoroughly tested for dimensions, sealing performance, strength, appearance, and functionality to ensure they meet pharmaceutical packaging requirements and customer specifications.
Step 04
In-Process Inspection
Continuous Monitoring During Manufacturing Our quality team performs regular inspections throughout the production cycle to verify dimensional accuracy, process consistency, and adherence to predefined quality parameters.
Step 05
Raw Material Inspection
Premium Materials, Verified Before Production Every batch of raw material undergoes comprehensive inspection for quality, purity, strength, and compliance before entering the manufacturing process, ensuring a reliable foundation for every product.
Step 06
Quality Policy
Committed to Uncompromising Quality We are dedicated to manufacturing pharmaceutical packaging products that consistently meet customer expectations and industry standards through continuous improvement, strict quality management systems, and process excellence.